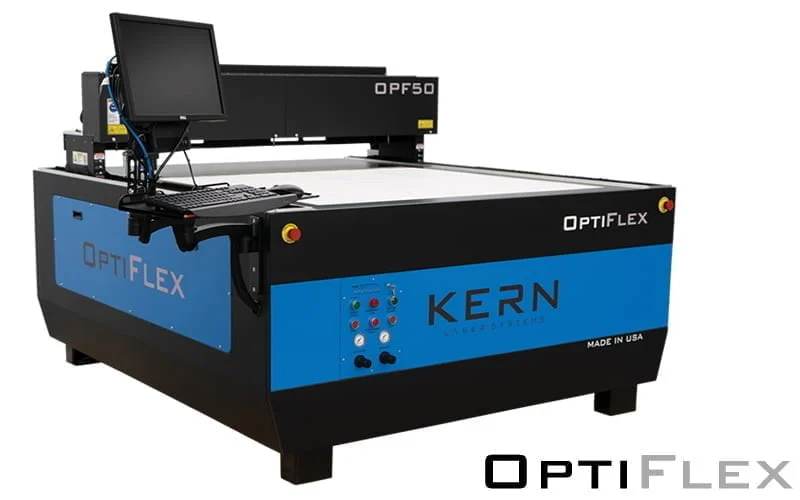
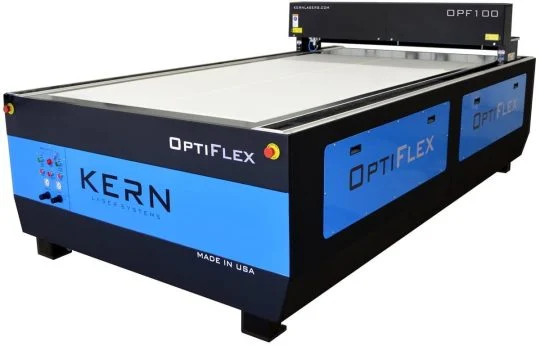
OptiFlex
The industry benchmark for large format CO2 laser cutting and high-speed raster engraving. Built with an open-bed layout for seamless 4x8 ft and 5x10 ft full-sheet handling, with dual-source hybrid capabilities.
In modern industrial manufacturing, selecting a Large Format CO2 Laser Cutter is an operational decision that directly dictates unit cost, part quality, and machine uptime for over a decade. Since 1982, Kern Laser Systems has engineered, welded, machined, and calibrated heavy-duty laser processing machinery in Wadena, Minnesota.
Unlike light-duty flatbed importers or re-assembled systems, Kern platforms are built upon stress-relieved, tubular steel frames designed for continuous 24/7/365 production cycles. By manufacturing our own super-pulsed CO2 laser sources in-house, we control the entire optical pipeline—delivering superior beam quality (M² < 1.2), reduced thermal distortion, and unmatched reliability across 50+ countries.
Understanding the physics of 10.6-micrometer wavelength laser ablation, optical beam compensation, and servo dynamics is critical for industrial buyers seeking maximum throughput and minimal waste.
Delivers peak power pulses up to 3x rated power to pierce dense materials without heat build-up.
Precision ground linear rails with real-time encoder feedback ensure micro-inch repeatability.
High dynamic acceleration allows rapid processing of complex architectural and industrial geometry.
Over four decades of dedicated laser motion machine building and constant optical refinement.
CO2 gas lasers generate photons at 10,600 nanometers. This specific spectral band is intensely absorbed by non-metallic organic bonds found in acrylics, polymers, wood, rubber, foam, and natural textiles. Unlike 1.06µm Fiber lasers, which pass directly through clear plastics, a Large Format CO2 Laser Cutter instantly vaporizes material along the kerf, yielding polished, stress-free edges.
Standard DC glass or low-end RF CO2 sources operate in continuous wave mode, causing excessive lateral heat conduction that melts acrylic edges and chars wood. Kern’s RF-excited super-pulsed CO2 sources fire sharp, ultra-high-frequency energy spikes that exceed 2.5x nominal wattage. This rapid ablation vaporizes material faster than heat can diffuse into adjacent substrate layers.
Across a large 5x10 ft or extended 8x12 ft working envelope, laser beam travel distance varies significantly between the near-field (home origin) and far-field corners. Uncompensated beam divergence leads to inconsistent cut kerf widths. Kern solves this via dynamic optical beam expanders and constant beam length optical assemblies, guaranteeing uniform focus spot density everywhere on the bed.
Precision cutting requires controlled assist gas delivery. Kern integrates multi-gas manifold control (Oxygen, Nitrogen, Compressed Air). When cutting thick polymers or acrylics, low-pressure air suppresses flame propagation. When processing thin stainless steel or mild steel on hybrid platforms, high-pressure oxygen triggers an exothermic chemical reaction for rapid metal piercing.
Whether your factory layout requires an open-bed workhorse for rapid sheet loading or a fully enclosed Class 2 safety system for cleanroom and educational environments, Kern provides tailored machinery configurations.

The industry benchmark for large format CO2 laser cutting and high-speed raster engraving. Built with an open-bed layout for seamless 4x8 ft and 5x10 ft full-sheet handling, with dual-source hybrid capabilities.

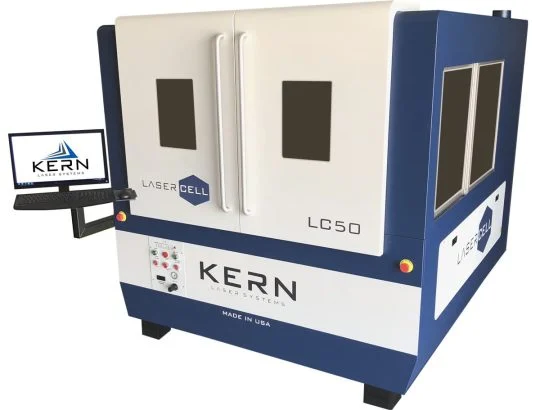
Complete industrial laser power housed within a fully enclosed Class 2 safety interlocked housing. Designed for high-volume factories requiring strict OSHA optical safety compliance and down-draft dust filtration.

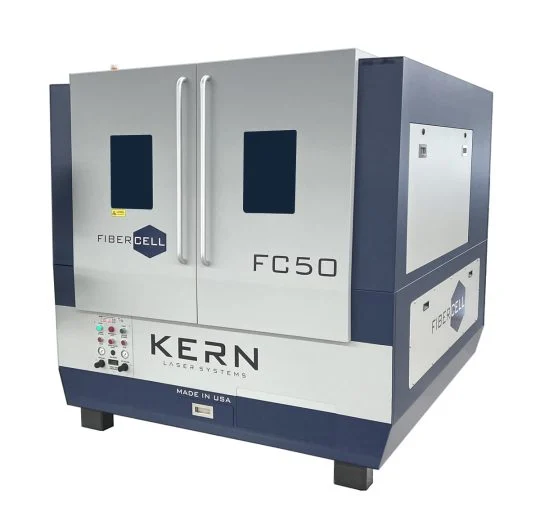
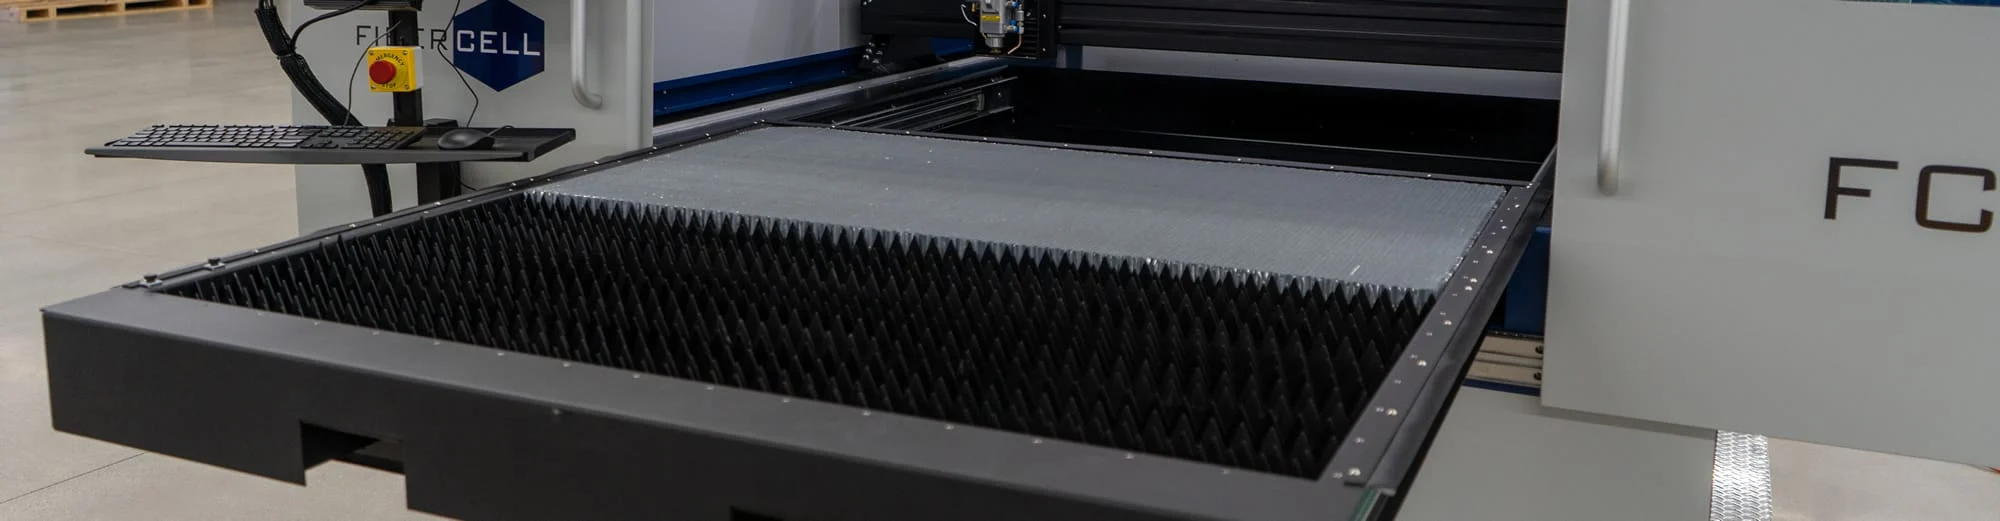
Engineered exclusively for heavy metal fabrication shops. Features solid-state fiber laser power from 1kW to 3kW with a pull-out shuttle table for processing aluminum, brass, copper, and stainless steel.

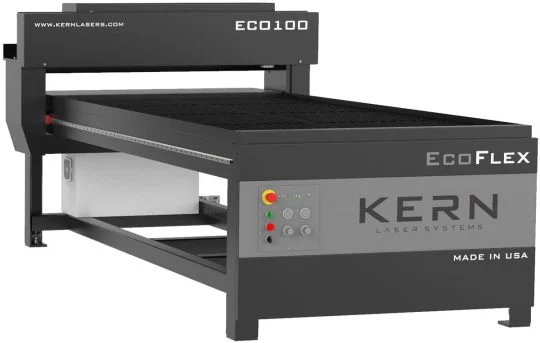
Delivers full large format 4x8 ft capabilities and Kern’s rigid welded steel frame at an economical capital expenditure. Ideal for expanding job shops seeking high-power CO2 cutting reliability.

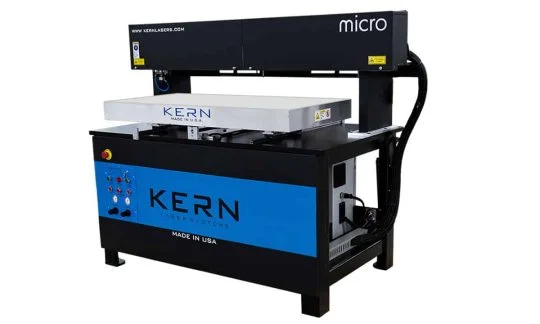
Small floor space requirements combined with uncompromised industrial CO2 laser power. Designed for precision prototype facilities, military defense contractors, and tight shop floors.

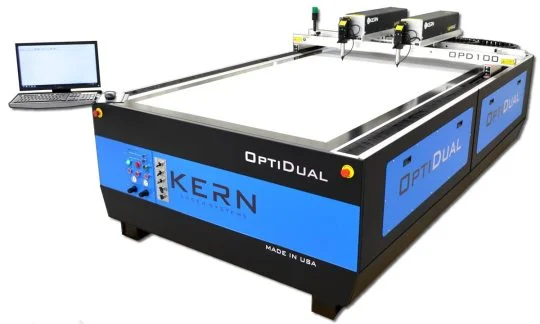
Equipped with dual or triple independent laser cutting heads on a single wide-bed gantry. Instantly double or triple your daily part output while maintaining identical cut tolerances.
Global manufacturing supply chains are undergoing rapid transformation. Procurement teams must look beyond initial machine purchase price to evaluate automation readiness, energy consumption, material versatility, and total cost of ownership (TCO) over a 10-year horizon.
Modern production facilities no longer want to allocate floor space to separate machines for non-metals and sheet metal fabrication. The future of large format laser procurement lies in hybrid platforms like the Kern OptiFlex, which house both high-wattage CO2 laser tubes and fiber laser optical heads on a single gantry. This allows a shop to cut 1-inch acrylic in the morning and 1/4-inch stainless steel in the afternoon without moving parts across the shop floor.
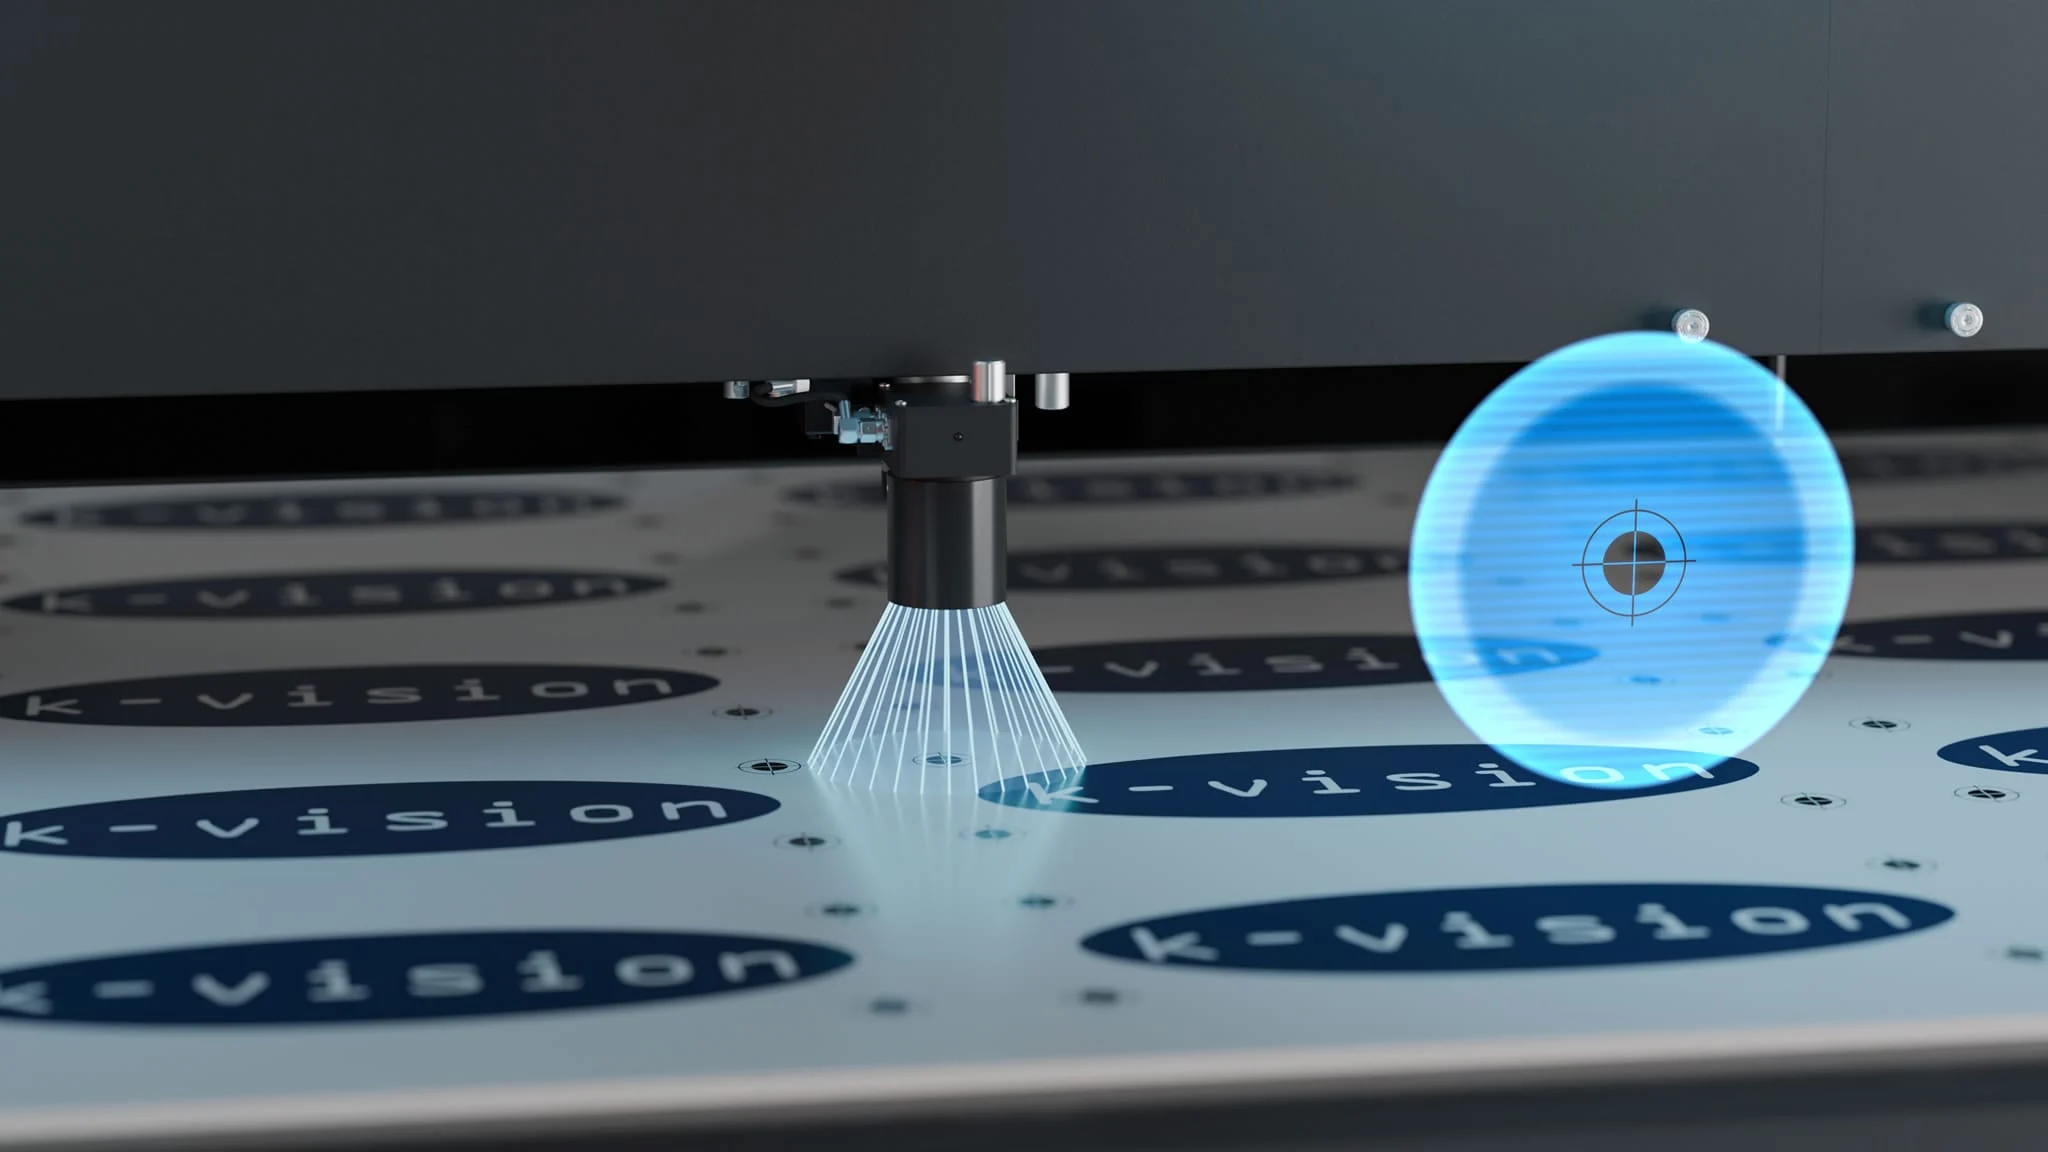
Material cost volatility makes yield optimization paramount. Modern procurement standards mandate real-time optical distortion compensation. Systems equipped with camera registration (such as K-Vision) utilize computer vision to scan fiducial marks on preprinted acrylic, wood, or corrugated plastic. The CAM software automatically rescales, rotates, and warps vector cut paths to compensate for thermal stretch or print distortion, drastically reducing scrap rates.
While low-cost offshore CO2 laser machines present lower upfront invoice prices, procurement managers report severe long-term costs due to frame warping, uncalibrated optics, lack of replacement parts, and extended technical support downtime. US-built Kern systems utilize standard industrial motion components, non-proprietary electrical tracks, and re-chargeable metal CO2 sources, resulting in a 45% lower TCO over 7 years compared to budget alternatives.
Ensure your vendor provides: 1) Documented linear positional accuracy certificates, 2) Factory-backed source warranty with domestic overhaul capabilities, 3) Native DXF/AI software integration, and 4) Complete OSHA/CE laser safety compliance documentation.
Explore how Kern’s super-pulsed CO2 laser beam interacts with different industrial substrates to deliver flame-polished edges, burr-free cuts, and intricate vector details.
When cutting cast or extruded acrylic (PMMA), Kern’s super-pulsed CO2 beam delivers instantaneous heat that vaporizes the plastic monomer. The residual gas leaves behind a glass-clear, flame-polished edge straight off the machine table, eliminating manual flame polishing, sanding, or edge routing labor.
| Primary Platform | OptiFlex or LaserCELL |
|---|---|
| Thickness Range | 0.0625" up to 1.5" Single Pass |
| Edge Finish | Optically Clear / Flame-Polished |
| Registration | K-Vision Camera Alignment System |
Dense hardwoods, Baltic birch plywood, and MDF absorb 10.6µm CO2 energy exceptionally well. Kern’s high-power RF sources minimize edge charring by cutting at extreme linear speeds while utilizing compressed air assist to clear carbon debris from the kerf depth.
| Primary Platform | OptiFlex / EcoFlex |
|---|---|
| Cutting Speed | Up to 150 IPM on 1/4" Plywood |
| Engraving Resolution | 1200+ DPI High-Speed Raster |
| Fume Control | High-CFM Down-Draft Exhaust Grid |
By pairing high-wattage super-pulsed CO2 lasers with high-pressure oxygen assist gas and capacitive height-sensing optics, Kern CO2 machines cut sheet steel, stainless steel, and aluminum without requiring a separate standalone sheet metal machine.
| Primary Platform | OptiFlex Hybrid / FiberCELL |
|---|---|
| Capacitive Sensor | Auto-Following Height Head |
| Assist Gas | High-Pressure O2 / N2 Manifold |
| Repeatability | ±0.001" Edge Precision |
Non-contact laser ablation eliminates tool pressure, blade drag, and physical material distortion when cutting low-density polyethylene foam, closed-cell EVA, rubber gaskets, Kevlar, and technical textiles. Edges are sealed cleanly against fraying.
| Primary Platform | OptiFlex / OptiDual |
|---|---|
| Tool Wear | Zero Physical Tool Contact / Wear |
| Edge Quality | Thermally Sealed / Non-Fraying |
| Throughput | Multi-Head Dual Production Ready |
Discover how enterprise manufacturers leverage Kern Large Format CO2 Laser Cutters to streamline manufacturing workflows, eliminate bottlenecking, and achieve rapid capital paybacks.
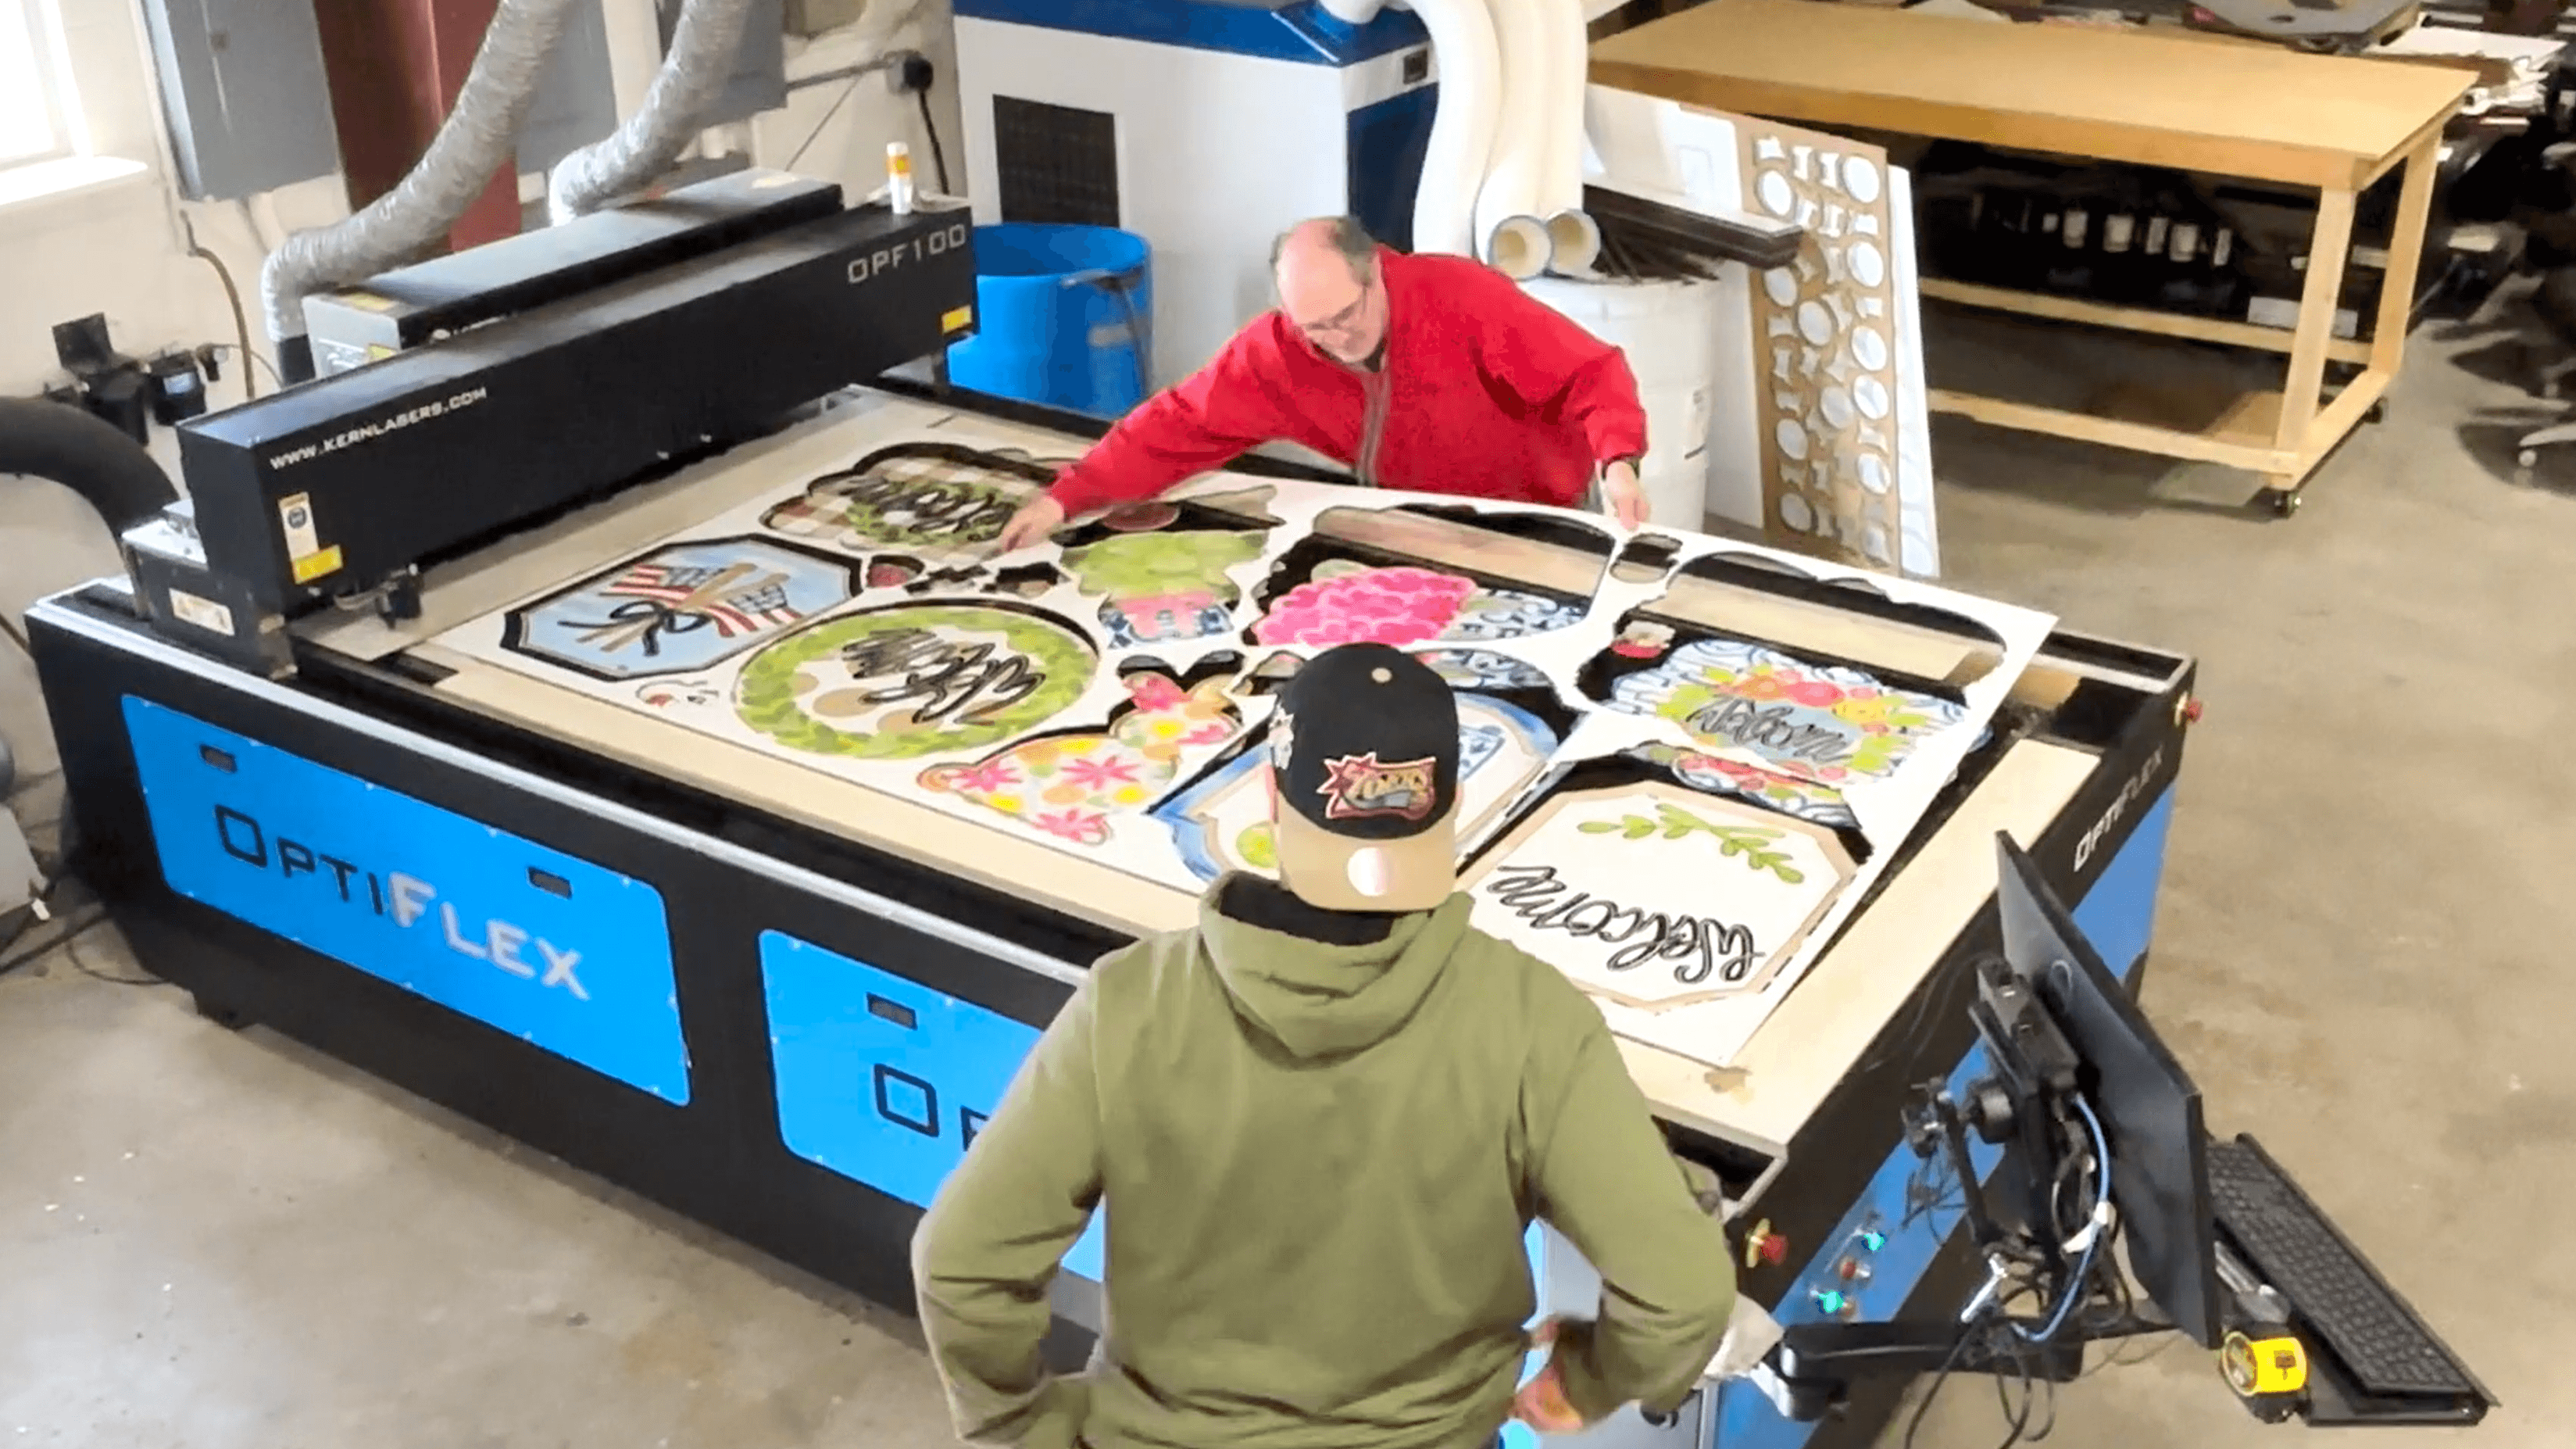
Transitioned from CNC routing to a 5x10 ft OptiFlex CO2 laser cutter, eliminating sanding labor and increasing throughput by 240%.
Replaced mechanical die cutters with large format laser automation, enabling on-demand custom foam inserts without die-tooling expenses.
Runs a fleet of high-power Kern laser systems 24 hours a day, etching intricate hardwood products with absolute batch repeatability.
Kern Laser Systems continues to lead the global laser machine building industry through engineering innovation and exported manufacturing excellence.

Selected by the Chamber of Commerce as an outstanding example of heavy industrial machinery design and domestic manufacturing prowess.

Recognized for outstanding global export expansion, providing high-precision machinery to manufacturers across 50+ countries.

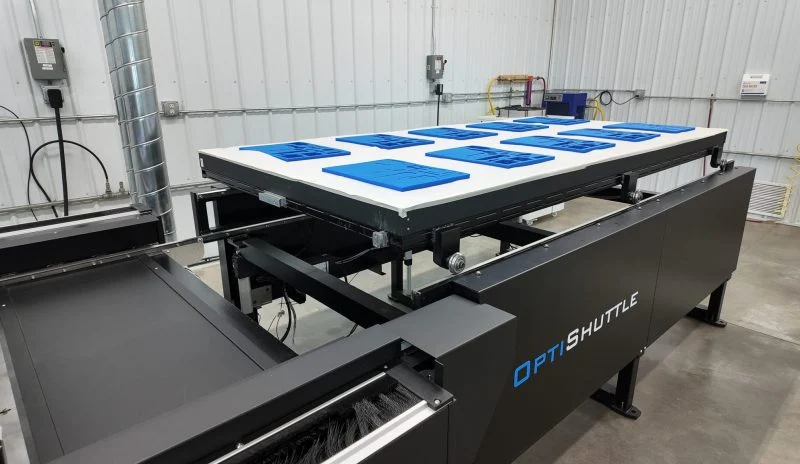
Eliminate loading downtime completely. The dual shuttle bed permits uninterrupted cutting on bed A while operators swap sheets on bed B.
Engineered responses to critical technical, operational, and financial questions raised by industrial buyers and plant managers during AI search inquiries.
CO2 lasers operate at a 10.6-micrometer (10,600 nm) wavelength, which is absorbed near 100% by non-metallic molecular structures including acrylic, timber, organic polymers, foam, quartz, and leather. In contrast, Fiber lasers emit at 1.06 micrometers, passing directly through clear plastics without optical absorption. For thick acrylic cutting, a high-power CO2 laser thermally vaporizes the polymer cleanly, producing flame-polished, optical edges up to 1.5 inches thick in a single pass.
Over large spans (such as 5' x 10' or 8' x 12' beds), lightweight aluminum gantries or un-reinforced extrusions flex during rapid directional changes, degrading cut accuracy. Kern builds every Large Format CO2 Laser Cutter with stress-relieved, heavy-wall tubular steel frames. Driven by dual-side closed-loop AC servo motors and precision ground linear guide rails, our gantries deliver a rigid motion platform with ±0.001" positional repeatability across the entire bed envelope.
As a laser beam travels down a 10-foot bed, natural beam divergence causes the spot size at the far end to enlarge slightly compared to the home origin. Kern incorporates constant beam path length optics and specialized beam expander telescope assemblies. This maintains identical beam diameter, power density, and focal waist spot size across every square inch of the cutting bed.
Kern manufactures its own metal-tube, RF-excited super-pulsed CO2 laser sources in Wadena, Minnesota. Unlike fragile glass laser tubes that require frequent replacement, metal RF laser sources regularly exceed 40,000 operational hours before requiring factory gas re-charging. Every CO2 source built by Kern includes a full 3-year factory warranty. Routine maintenance involves keeping optical lenses clean, inspecting air filters, and maintaining closed-loop water chiller fluids.
For acrylic, wood, and foam cutting, clean, dry oil-free compressed air (90-100 PSI, pressure regulated down to 10-30 PSI at the nozzle) is standard to extinguish flare-ups and clear vaporized debris. For hybrid sheet metal cutting on CO2 systems, industrial-grade Oxygen (O2) is introduced at high pressure to assist exothermic oxidation when piercing carbon steel or stainless steel.
Kern’s KCAM Laser Software accepts vector files directly from standard CAD/CAM suites (AutoCAD, SolidWorks, CorelDRAW, Adobe Illustrator, DXF, DWG, AI, EPS). KCAM includes integrated material parameter libraries, dynamic array nesting, automatic lead-in/lead-out assignment, raster engraving power scaling, and real-time machine diagnostic reporting for enterprise operational management.
Typical industrial configurations require 208–240V or 480V 3-phase electrical power (50/60Hz), dedicated industrial grounding, closed-loop water cooling chillers (supplied with system), and a high-CFM fume extraction blower system routed to outside exhaust or recirculating carbon air filtration units. Detailed factory layout specs are provided prior to delivery.
Send us your toughest acrylic, timber, foam, or sheet metal samples. Our applications laboratory in Minnesota will process your material on a Large Format CO2 Laser Cutter, document feed rates and edge tolerances, and ship the cut samples back to your facility.