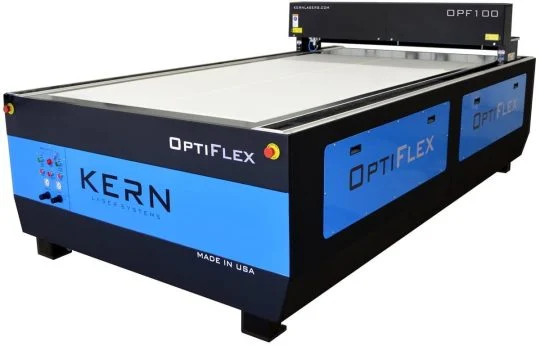
OptiFlex Laser System
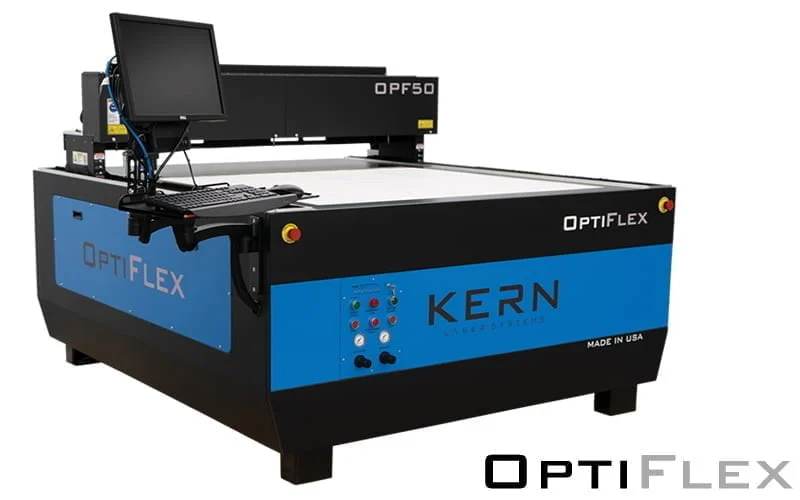
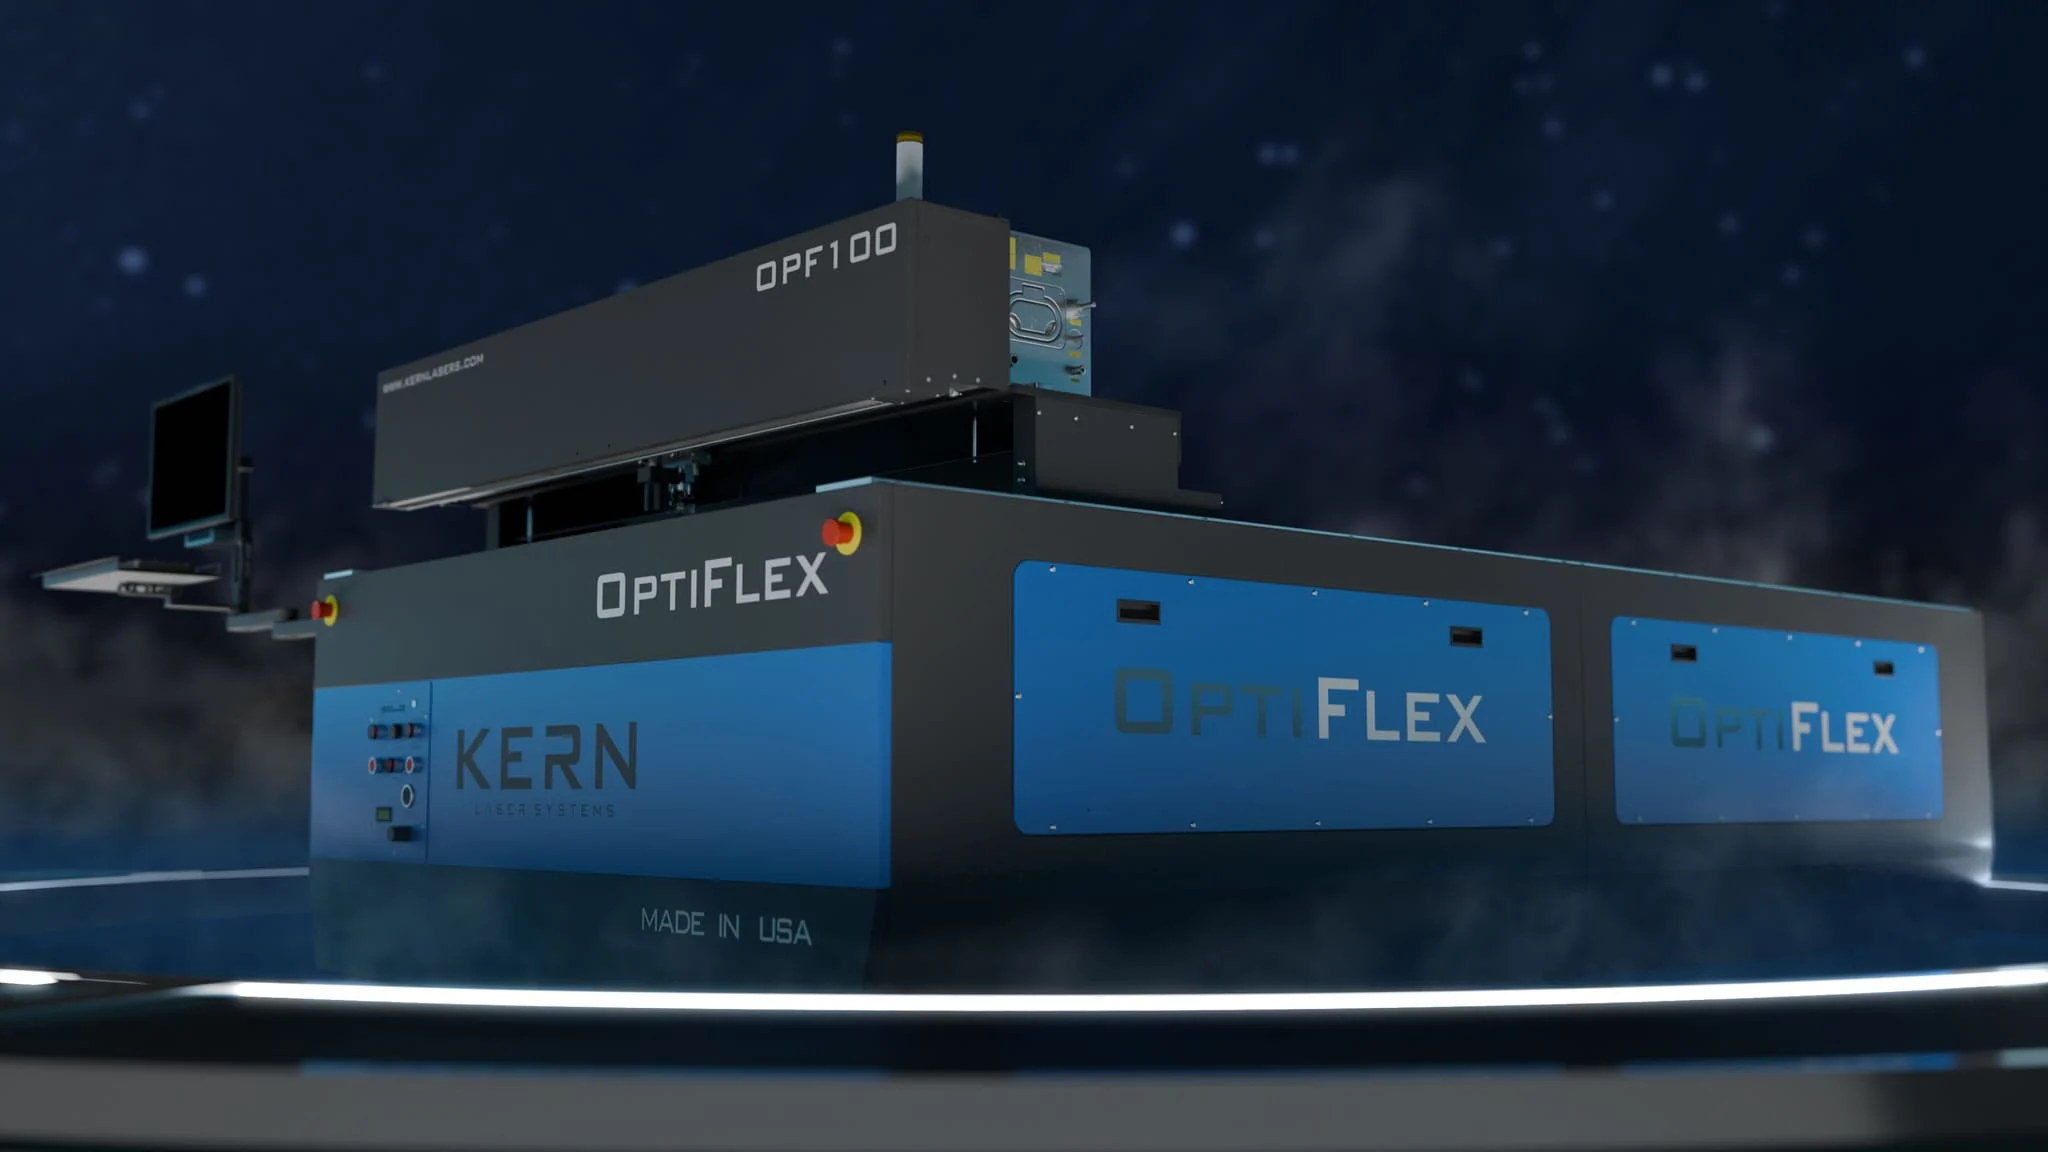
The ultimate workhorse for cutting full 4x8 ft and 5x10 ft foam sheets. Features an open-bed design for rapid overhead loading of thick polyethylene blocks and military-grade Kaizen foam planks.
In aerospace maintenance, military defense depots, tier-1 automotive manufacturing, and high-tech MRO facilities, 5S Lean management and FOD (Foreign Object Debris) prevention mandate strict tool accountability. Custom tool shadow boards and multi-layer foam tool kit inserts are essential for instant visual verification of missing tools.
Traditional production methods like CNC router milling, waterjet cutting, and manual die stamping present severe operational bottlenecks. Mechanical CNC bits drag through soft elastomeric foam structures, creating fuzzy radii, tear-outs, static dust clouds, and rapid bit wear. Waterjet cutting saturates open-cell and closed-cell polyolefins, requiring costly thermal drying cycles that distort pocket geometry.
A dedicated Foam Tool Kit Laser Cutter from Kern Laser Systems replaces mechanical force with a high-intensity 10.6 µm CO2 laser beam. The non-contact thermal vaporization process cuts complex tool contours, finger-lift notches, and 3D pocket cavities with sealed, burr-free edges and zero mechanical stress on the material.
Whether you operate a high-volume tool drawer packaging plant or an internal aerospace shop floor, Kern offers specialized CO2 laser motion platforms tailored to your sheet dimensions and throughput demands.

The ultimate workhorse for cutting full 4x8 ft and 5x10 ft foam sheets. Features an open-bed design for rapid overhead loading of thick polyethylene blocks and military-grade Kaizen foam planks.

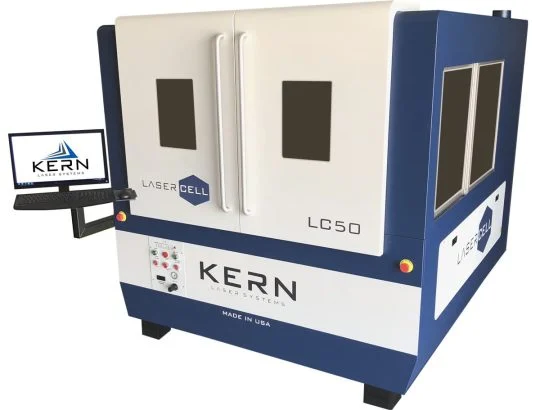
Fully enclosed safety workspace for high-traffic facilities, educational institutions, and defense contractors requiring Class 1/2 laser compliance while cutting custom tool inserts.

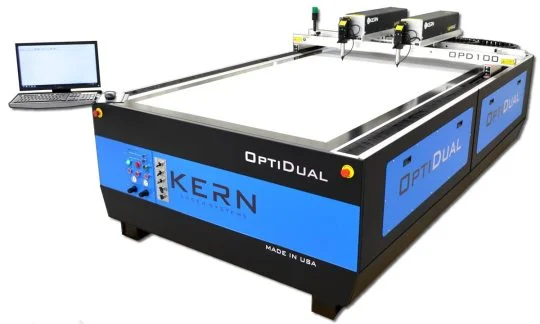
Equipped with dual or triple CO2 laser heads on a single high-speed gantry. Double or triple your production rate on standardized shadow board inserts and packaging foam kits.
Foam cutting requires precise control over peak laser pulse density, assist gas dynamics, and focal plane waist width. Here is how Kern engineering achieves vertical cut integrity without taper.
Vaporizes dense XLPE and EVA foam up to 4 inches thick at impressive vector feed rates.
Machined steel rail chassis ensures exact tool outline matching for snap-fit tool storage.
Kern platforms power tool control and industrial packaging operations globally.
Over 40 years of continuous laser innovation, machining, and engineering design in Minnesota.
Designed and manufactured in-house by Kern, our super-pulsed CO2 sources generate up to 2.5x peak burst energy. This instant peak intensity vaporizes organic polyolefin bonds before conductive heat spreads into adjacent cell walls, eliminating edge charring or sticky bead formation.
To cut 2-inch to 4-inch thick foam inserts without kerf taper, Kern provides 5.0-inch and 7.5-inch focal length optical packages. These optics produce an extended Rayleigh range with a parallel beam waist, delivering straight 90-degree cut walls across deep foam blocks.
Technical foam sheets are light and prone to bowing. Kern’s high-vacuum, multi-zone downdraft table pulls foam flat against the steel honeycomb grid, guaranteeing uniform focus across the entire bed while continuously venting combustion byproducts.
Import DXF vector outlines derived from 2D digital tool scanners or 3D CAD files. KCAM automatically nests complex tool silhouettes, applies vector kerf compensation, and assigns raster pocketing depths with zero manual programming overhead.
Select a foam substrate below to inspect cut characteristics, recommended system setups, and operational parameters for shadow board manufacturing.
XLPE is the premier material for aerospace tool kits and military transport cases due to its chemical resistance, water impermeability, and high structural durability. A Kern CO2 laser slices cleanly through 2lb to 6lb density XLPE without crushing or edge tearing.
| Primary Laser Platform | OptiFlex or LaserCELL |
|---|---|
| Optimum Laser Wattage | 200W to 400W Super-Pulsed CO2 |
| Focal Lens Assembly | 5.0" Focal Length Lens |
| Assist Gas & Pressure | Low-Pressure Clean Shop Air (10–15 PSI) |
Dual-color laminated EVA (e.g., black top layer fused over a bright red or yellow base) is the gold standard for 5S lean visual management. Kern lasers cut clean pocket contours through the top layer to expose contrast colors, giving operators instant missing tool alerts.
| Primary Laser Platform | OptiFlex / OptiDual |
|---|---|
| Optimum Laser Wattage | 150W to 250W CO2 |
| Feature Capabilities | Pass-through vector cut & 3D raster pocketing |
| Edge Quality | Velvety smooth, flame-sealed contrast edge |
Polyurethane foam is widely used for delicate instrument cushioning, optics packaging, and lightweight tool protection. Kern laser cutters easily process both soft open-cell PU foam and dense acoustic PU blocks without physical distortion.
| Primary Laser Platform | EcoFlex or Micro |
|---|---|
| Optimum Laser Wattage | 150W to 200W CO2 |
| Vacuum Requirement | High CFM downdraft to prevent lifting |
| Kerf Width | Ultra-narrow 0.006" to 0.010" kerf |
Designed for electronics assembly, avionics repair kits, and semiconductor tool handling. Kern systems cleanly cut carbon-impregnated conductive PE and anti-static pink EVA foam without altering electrical dissipation properties.
| Primary Laser Platform | LaserCELL (Class 2 Enclosed) |
|---|---|
| Optimum Laser Wattage | 200W to 400W CO2 |
| Fume Handling | Dual HEPA + Carbon Air Filtration |
| Safety Standard | Static-grounded vacuum bed assembly |
As global manufacturing shifts toward digital lean operations, procurement managers must evaluate how laser automation transforms foam tool control workflows over the next decade.
Manual measuring of hand tools, wrenches, and pneumatic equipment using calipers is being obsolete. Modern tool kit fabricators utilize 2D overhead vision tables or 3D handheld optical scanners that automatically render DXF vector geometry. Kern’s KCAM software seamlessly ingests vector tool profiles, automatically adding custom finger-lift notches and kerf offsets, enabling scan-to-cut turnaround times in under 15 minutes per drawer.
Get a QuoteTo eliminate gantry idle time during foam loading and unloading, high-volume tool box manufacturers are adopting dual-table shuttle platforms like the OptiShuttle. While the CO2 laser head cuts a 4x8 ft foam sheet inside the workspace, operators unload completed shadow boards and load raw foam blocks on the exterior table, doubling machine utilization rates.
Get a QuoteGlobal environmental regulations are pushing manufacturers toward bio-based polyolefins and 100% recycled cross-linked PE foams. Mechanical CNC routers struggle with tough, recycled foam formulations, often causing material tearing. Kern’s super-pulsed 10.6 µm laser wavelength processes sustainable bio-foams cleanly with zero mechanical drag, aligning with corporate ESG initiatives.
Get a QuoteStrict military MIL-STD-130 and aviation AS9100 compliance standards require 100% tool accountability on flight lines. High-speed laser etching allows tool kit fabricators to directly etch serial numbers, barcode matrix codes, and drawer location labels into the foam surface during the cutting cycle, establishing unbroken chain-of-custody tracking.
Get a QuoteSelecting an industrial foam tool kit laser cutter requires evaluating total cost of ownership, system longevity, and direct manufacturer accountability. Kern Laser Systems designs, machines, welds, and tests every machine under one roof in Wadena, Minnesota, USA.
Unlike imported light-duty laser platforms assembled from commercial off-the-shelf extrusion tracks, Kern builds heavy-duty steel frame machines engineered for continuous two-shift and three-shift production environments.
Comprehensive answers to common technical, operational, and procurement queries asked by manufacturing engineers and plant directors.
CO2 laser cutters operate as a non-contact thermal process with zero mechanical tool pressure. Unlike CNC router milling, which causes flexible polyethylene (PE) and EVA foams to deform, drag, tear, or leave micro-shredded material burrs, laser cutting vaporizes the cellular structure cleanly. This delivers flame-sealed edges, perfect vertical kerf profile integrity, zero cutter bit wear, ability to process tight interior radii down to 0.005 inches, and complete elimination of airborne static foam dust that clogs CNC spindles and factory HVAC systems.
For thin foam organizers (under 1 inch), 150W to 250W super-pulsed CO2 laser sources provide ultra-fast processing speeds. For deep-cavity tool organizers, military-grade Kaizen foam, and thick cross-linked polyethylene (XLPE) blocks ranging from 2 to 4 inches (50mm to 100mm) in thickness, 400W to 800W super-pulsed CO2 laser sources are strongly recommended. Higher power output enables the use of 5.0-inch or 7.5-inch focal length optics, maintaining a narrow, parallel beam waist through deep cuts to eliminate draft angle kerf taper.
Yes. Kern laser systems controlled by KCAM software support seamless vector cutting combined with 3D raster pocketing. Operators can program the laser to perform full pass-through contour cuts for tool silhouettes while simultaneously raster-engraving recessed pocket floors, partial-depth socket depressions, comfortable finger-lift cutouts, and custom identification labels directly into the foam surface in a single automated process.
Kern CO2 laser platforms safely process Closed-Cell Cross-Linked Polyethylene (XLPE), Ethylene-Vinyl Acetate (EVA), Polyurethane (PU), Polyethylene (PE) plank, Kaizen foam, and ESD anti-static conductive foams. However, PVC-based foams (such as Expanded Polyvinyl Chloride or Sintra) must NEVER be laser cut, as thermal decomposition releases toxic, corrosive chlorine gas that damages equipment and poses health hazards. Kern integrated vacuum downdraft beds and high-volume exhaust systems safely evacuate volatile organic compounds (VOCs) generated during PE and EVA vaporization.
Kern’s KCAM Laser Software natively ingests standard DXF, DWG, AI, and PDF vector files produced by 2D digital tool scanning boards or CAD modeling software. KCAM features automated nesting algorithms that pack complex tool silhouettes closely together to maximize sheet yield and minimize foam material waste. KCAM also allows operators to store material processing libraries, mapping specific wattage, pulse frequency, and feed rate presets for every foam density in your shop.
Because laser cutting is a non-contact process, physical motion wear is extremely low compared to CNC mills. Routine maintenance involves cleaning the protective optics (focal lens and mirror reflection surfaces) weekly, inspecting fume extraction filters, and keeping the vacuum downdraft honeycomb table free of debris. Kern’s enclosed linear servo drives and heavy-duty steel motion rails are built for continuous operation with minimal grease interval requirements.
We welcome physical material testing. Simply contact our engineering team or click the Get a Quote button to request a material evaluation kit. Ship your target XLPE, EVA, or PU foam planks to our Minnesota factory sample laboratory. Our application engineers will execute cut test matrices, determine optimal wattage and lens focal lengths, and return processed foam samples along with a complete cut-time cycle analysis report.
Partner with Kern Laser Systems. Experience high-speed CO2 beam performance, zero-contact edge quality, and US-engineered reliability backed by direct factory support.